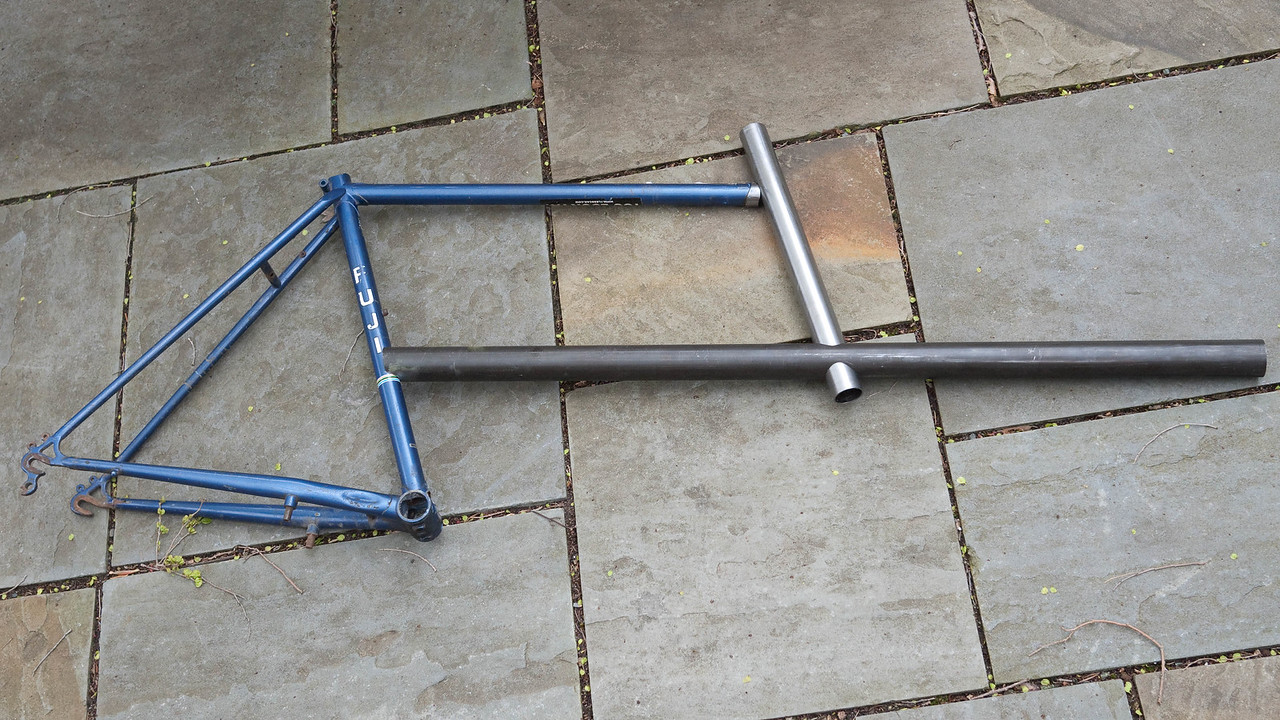
Hi, I’m trying to extend the headtube of an old mtb to do a cycle truck style build (will also be adding a support from downtube to extension), but I’m struggling to find a US supplier with a tube suitable for the inner sleeve of the extension. I was hoping for OD of greater than 28.6mm/radial gap smaller than .7mm, maybe 29.something with >=1.5mm walls, as the mtb is a 1" steerer with ISO/30mm headtube ID. I’m relatively new to frame building and do not have the best intuition on tolerances, so maybe I’m worrying about nothing, but .7 seems like to loose a fit for bronze brazing in this application.
If you have a lathe, make the extension like what Ti Cycles used to sell,
only make yours in steel (duh) and braze it in. Dave’s was intended for a press fit, no brazing.
If you don’t have a lathe, I pity you. How can a man live without a lathe? I guess one way is make friends with someone who has one. Maybe there’s some forum where you could find someone with a lathe? Hmm.
Here’s mine, not from Ti Cycles but inspired by theirs:
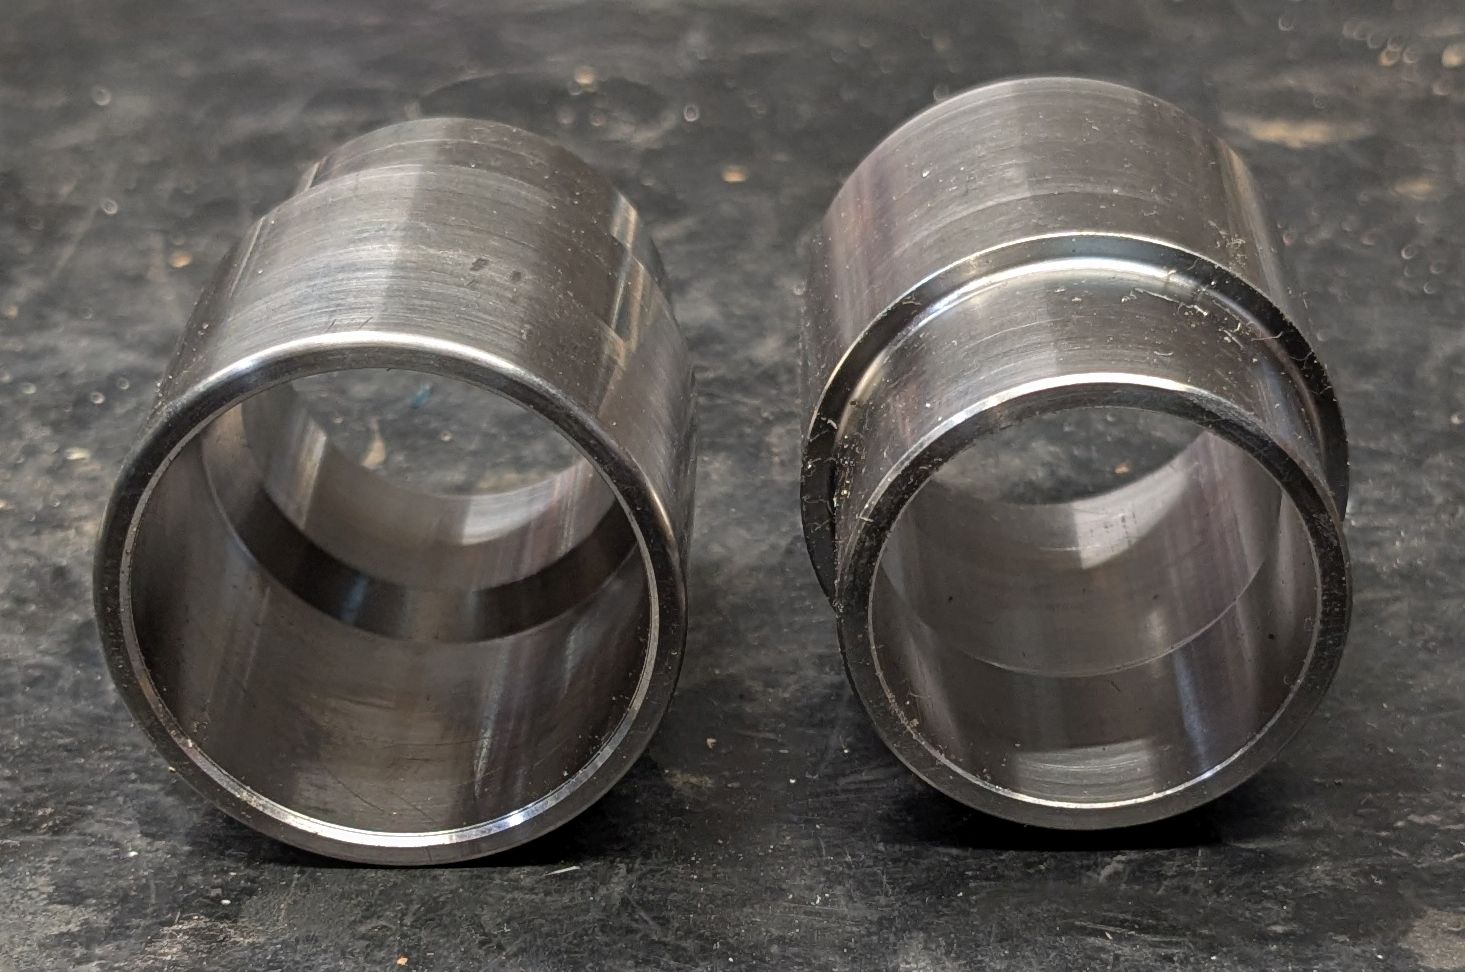
Note, I am not volunteering, too much on my plate. But it’s not a very complex part, shouldn’t be too hard to get one made.
1 Like
I appreciate the sympathy, maybe someday I shall have a lathe of my own. If I do find someone with a lathe, what OD range should I shoot for?
Way back for my first couple cycletruck conversions, when tooling was scarce but time wasn’t, I sacrificed the original steel headset cup but chopping off the flared portion and filing it flush with the sides til was uniform. Then I’d remove the paint (they were old and cheap) and carefully press it in, ensuring the overlap was equal in both the old HT and new HT extension.
It was far from ideal, but worked well with what I had at hand.
Triangulating the bottom of the extension back to the downtube reduced a lot of the forces on that joint, at least enough that its minimal length didn’t seem to present issues, or at least I had zero breaks in an admittedly small sample size.
Good luck!
I see what you mean now by a cycle truck extended headtube, triangulated to the downtube. I think my proposed method doesn’t make as much sense for that. I was thinking the small extension to the top of the headtube that some riders want for getting the bars higher.
That lathe-turned piece would need a lot of metal removed, for how long an extension your frame needs. A short internal sleeve like you’re talking about is more efficient use of time and materials.
Make it a snug sliding fit ~.001 - .002 on the diameter for 56% silver, and double that for brass. Any extra slop is giving the part an opportunity to move on ya. Snugger is more self-jigging.
1 Like
If you cant find a tube of the exact diameter or machine one you could take the closest size up and make two cuts lenght wise and close it down to reach the right od.
Ideally you’d then weld it shut, file it smooth and braze it as a sleeve, but brazing as is with the slit facing back might work too, make sure you get full penetration all around and put a brace from the downtube to the new head tube section
1 Like
Yes, this is often the best way to make acceptable tubes of a given size. You can also cut a section out, open it up a bit, and graft in a piece from another bit of the same tube. This is how I make crown race seats (which do need a little bit of finishing on the minilathe, but it’s minimal, and no boring).
would I also be able to do a single slit and rely on the expansion of the tube on the inside?
If you’re using a size too small you mean? Yes but you’ll have a wider section without sleeve. To be clear you’re not cutting it in halves, the two cuts are next to each other, to remove some of the circonference